
Services · Non-Destructive Testing
Heat Exchanger, Chillers and Tube Inspection
A single condenser or steam generator holds several thousand tubes, and one leak takes the unit down. High-speed electromagnetic and rotary ultrasonic scanning finds the corroded, eroded and cracked tubes inside the outage window.
Request a Quote
In brief
TCR Engineering inspects tubular products in heat exchangers, chillers, condensers and boilers by non-destructive testing (NDT), including Eddy Current Testing (ECT), Remote Field Eddy Current Testing (RFET), Magnetic Flux Leakage (MFL), and Internal Rotary Inspection System (IRIS). These techniques utilise internal diameter probe coils, such as bobbin coils, for testing both non-ferrous and ferrous materials (the latter with magnetic saturation).
Overview
TCR inspects the heat exchangers, condensers and steam generators common in power plants for corrosion, erosion, cracking and other material degradation. These tubular structures, which contain thousands of tubes, must be regularly monitored to prevent leaks and ensure operational integrity.
- Assets: heat exchangers, condensers and steam generators, which carry thousands of tubes each.
- Detects: corrosion, erosion, cracking and other material degradation.
- Speed: high-speed testing identifies anomalies accurately and minimises downtime.
- Standards: ASTM E243 for eddy current, and ASME Boiler and Pressure Vessel Code Section V for ultrasonic and eddy current examination of tubing.
The high-speed testing provided by these methods ensures accurate identification of anomalies and minimises downtime.
The testing is conducted in accordance with relevant international standards, such as ASTM E243 for eddy current testing and ASME Boiler and Pressure Vessel Code, Section V for ultrasonic and eddy current examination of tubing. The work serves power generation and industrial plants.
Eddy Current Testing
TCR Engineering offers Eddy Current Testing (ECT), a fast and highly accurate technique for detecting discontinuities in tubing, heat exchangers, condensers, steam generators, air coolers, and feedwater heaters. Using electromagnetic induction, TCR detects flaws in conductive materials, including small near-surface cracks.
This method requires minimal surface preparation and can easily accommodate complex geometries, making it ideal for a wide range of industrial applications.
In addition to flaw detection, ECT is effective for alloy separation, determining heat treatment conditions, measuring electrical conductivity, and assessing coating thickness. It can also pinpoint the location of repair welds, girth welds, and seam welds on ground-machined surfaces.
TCR Engineering’s in-house team of certified Eddy Current Testing professionals inspects tubing in heat exchangers and other critical equipment. The instruments are portable and contactless and give instant feedback, which keeps downtime short. The instrument is the Olympus (Evident) MultiScan MS5800: 20 Hz to 6 MHz for eddy current, and 20 Hz to 250 kHz for remote field and near field testing, at an inspection speed of 2 metres per second.
Key Benefits of TCR Engineering's Eddy Current Testing Services:
- High-Speed and Precise Detection: Rapid flaw identification with minimal surface preparation.
- Complex Geometries: ECT can investigate intricate shapes and sizes.
- Non-Destructive: Ensures the integrity of the material without physical damage.
- Versatility: Can detect flaws, measure conductivity, and identify different alloys.
- Immediate Feedback: Portable, real-time inspection results to facilitate quick decision-making.
Applicable Standards:
- ASTM E243: Standard Practice for Electromagnetic (Eddy-Current) Testing of Tubular Products
- ASME Section V: Non-Destructive Examination (NDE), covering Eddy Current Testing for heat exchanger tubes
- ISO 15548: NDT equipment and techniques for eddy current testing
TCR Engineering ensures that all tubes are properly cleaned prior to testing, with hydro jetting at pressures ranging from 280 to 560 kg/cm². The adequacy of cleaning is verified by inserting a dummy probe or rod to guarantee smooth inspections.
Eddy current technicians evaluate each flaw signal against calibration standards, to the standards listed above.
Remote Field Eddy Current Testing (RFET)
TCR Engineering offers Remote Field Testing (RFET), an advanced electromagnetic non-destructive testing (NDT) method as per ASTM E2096 and ASME Section V, ideal for detecting and sizing wall thinning due to corrosion, erosion, wear, pitting, and baffle cuts in ferromagnetic tubes.
- Standards: ASTM E2096 and ASME Section V.
- Detects and sizes: wall thinning from corrosion, erosion, wear, pitting and baffle cuts.
- Materials: ferromagnetic tubes.
- Equipment served: boilers, feedwater heaters, air coolers and carbon steel heat exchangers.
- Combined technique: RFET with Near Field Testing, deployed singly or together depending on the equipment and the condition of the asset.
Our RFET services are widely utilised in critical industrial equipment such as boilers, feedwater heaters, air coolers, and carbon steel heat exchangers, providing accurate assessments of tube integrity without the need for invasive procedures.
We combine Remote Field Eddy Current Testing (RFET) and Near Field Testing (NFT), deploying them individually or together, depending on the specific capabilities of the testing equipment and the condition of the asset. These methods allow us to achieve comprehensive coverage, ensuring reliable detection of both surface and subsurface defects.
Magnetic Flux Leakage Testing (MFL)
TCR Engineering offers Magnetic Flux Leakage (MFL), an electromagnetic non-destructive testing (NDT) technique used to detect corrosion, pitting, and other forms of material loss in steel structures and ferromagnetic tubing. MFL is widely employed in critical industrial applications, including pipelines, storage tanks, and heat exchangers.
MFL uses a strong magnet to magnetise the ferromagnetic material under test. When defects like corrosion or material thinning are present, the magnetic field "leaks" from the surface, and the sensors detect and measure the extent of wall loss.
Key Benefits of TCR Engineering's MFL Services:
- Accurate Detection of Defects: MFL is ideal for identifying sharp defects such as pitting, grooving, and circumferential cracks.
- Effective for Ferromagnetic Tubing: This method is suitable for detecting defects in steel and other ferromagnetic materials.
- Aluminium-Finned Carbon Steel Tubing: MFL is highly effective even in aluminium-finned carbon steel tubes, as the magnetic field remains largely unaffected by the fins.
- Complementary to Remote Field Eddy Current Testing (RFET): MFL provides a back-up inspection to RFET, ensuring a comprehensive evaluation of tube integrity.
By using TCR Engineering's advanced MFL services, industries can detect and mitigate corrosion and material loss early, enhancing asset longevity and reducing operational risks.
Internal Rotary Inspection System (IRIS)
TCR Engineering provides Internal Rotary Inspection System (IRIS), a highly accurate ultrasonic method for the non-destructive inspection of tubes, particularly in heat exchangers, boilers, and condensers. The IRIS technique uses an ultrasonic beam to measure and detect metal loss on both the inner and outer walls of the tube.
The IRIS probe is inserted into a water-filled tube, and as it is pulled out, real-time data is displayed and recorded, allowing precise wall thickness measurement and defect detection.
Key Benefits of TCR Engineering's IRIS Services:
- Precise Defect Detection: IRIS can accurately detect and measure metal loss along both the length and circumference of the tube, providing a comprehensive evaluation of tube integrity.
- High Accuracy for Ferrous Materials: IRIS offers superior accuracy for measuring wall thickness in ferrous materials, with a resolution as low as 0.15 mm, making it more accurate than Remote Field Eddy Current Testing (RFET) for ferrous tubes.
- Comprehensive Analysis: This method is highly effective at detecting both internal and external corrosion, erosion, and other forms of degradation, making it ideal for asset integrity management.
Limitations:
- Slower Testing Speed: While IRIS offers high accuracy, it is slower compared to other techniques, with a scanning speed of approximately 1 inch per second, making it less efficient for large-scale inspections.
- Surface Cleaning Requirement: IRIS requires thorough cleaning of the tube surface, often more rigorous than what is required for Eddy Current Testing (ECT).
- Despite its slower speed, IRIS provides high accuracy in wall thickness measurement, making it a critical method for industries focused on the longevity and reliability of their tubular assets. TCR Engineering’s experienced team ensures precise inspections that help prevent unexpected failures and extend the life of your equipment.
Fully Saturated Eddy Current Testing
TCR Engineering offers Saturation Eddy Current (SET), a specialised non-destructive testing technique used for inspecting thin ferromagnetic materials such as carbon steel (CS), duplex stainless steel, and slightly magnetic materials like Monel Nickel-Copper alloys.
This advanced method is highly effective for detecting and quantifying both internal and external cracks, as well as local defects and overall wall loss in ferromagnetic tubes used in boilers, feedwater heaters, air coolers, and carbon steel heat exchangers.
This technique, done in accordance with ISO 15548-1 and ASME Section V, identifies both internal and external cracks, pitting, and wall thinning in challenging materials, providing detailed insights into the condition of tubes.
SET is particularly beneficial in industries like power generation and petrochemical processing, where the reliable operation of critical heat exchangers and boilers depends on early detection of material degradation.
TCR Engineering’s use of Saturation Eddy Current ensures precise inspections, enabling operators to avoid costly downtime and prevent unexpected failures.
Saturation eddy current inspection is fast and accurate, and the early warning it gives helps extend the life of critical components.
Specialised electromagnetic methods for shell-and-tube heat-exchanger inspection.
| Method | Application | Standards |
|---|---|---|
| Eddy Current Testing (ECT) | Non-ferrous tubes (Cu, brass, admiralty, stainless steel) | ASTM E690, ASME V Article 8 |
| Eddy Current Array (ECA) | Faster 2D scanning of tube and tube-sheet bores | ASTM E2884, ASME V Article 8 |
| Remote Field Eddy Current Testing (RFET) | Ferromagnetic tubes (carbon steel, low-alloy steel) | ASTM E2096 |
| Internal Rotating Inspection System (IRIS) | High-resolution ultrasonic wall-thickness mapping | ASME V Article 23 |
| Near-Field Testing (NFT) | Finned air coolers (fin-fan) | Written procedure qualified on reference tubes (no consensus standard covers NFT) |
| Surface ECT (SECT) | Through-coating crack detection on fin tubes | EN 1711 |
Tube-by-tube condition maps and remaining-life estimates. Reformer pigtail and inlet-outlet manifold inspection covered under the same crew. Anchor clients include refineries, fertiliser plants, petrochemical complexes, fossil-power and waste-heat boilers, and process plants in chemicals and steel.
Standards: ASTM E690 (in-situ eddy current examination of non-magnetic heat exchanger tubes), ASTM E2884 (eddy current sensor arrays) and ASTM E2096 (remote-field testing of tubular products).
Eddy current testing on video
Related insights
4 published insights on this site bear directly on Heat Exchanger and Tube Inspection. They are below; the full index carries all 79 Non-Destructive Testing insights.
-
TCR's 50 Years of Heat Exchanger Tube Testing Expertise
Eddy Current Testing reveals wall thinning in heat exchanger tubes before failure. TCR's 50+ years of probe inventory ensures complete coverage.
-
Reformer Tube Inspection Services Petrochemical: Why Your Plant's Future Depends on Getting This Right
ARTiS revolutionises reformer tube inspection with Level III FFS assessment per API 579, predicting failures months ahead of traditional methods.
-
Protect Your Heat Exchangers with TCR's World-Class Tube Inspection Services
Ensure your heat exchangers run at peak performance! Trust TCR Engineering for tube inspections with rapid mobilisation and current-generation NDT
-
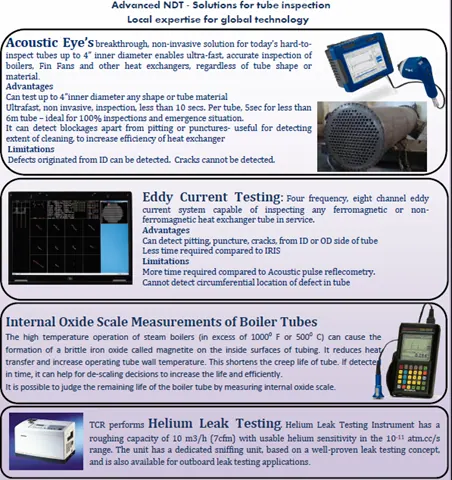
TCR’s Advanced NDT Solutions for Tube Inspection
Undertaking Acoustic Eye, Eddy Current, Oxide Scale Measurement and Helium Leak Test
Read all 79 Non-Destructive Testing insights →All insights →
Frequently asked questions
Which method suits which tube material?
Eddy current testing suits non-ferrous tubes such as copper, brass, admiralty and stainless steel. Remote field testing covers ferromagnetic carbon and low-alloy steel tubes. Near-field testing handles finned air coolers, magnetic flux leakage works on aluminium-finned carbon steel, and saturation eddy current addresses duplex stainless steel and Monel.
When is IRIS preferred over remote field testing?
IRIS is preferred where precise wall thickness measurement matters, offering resolution down to 0.15 mm on both inner and outer tube walls, which is more accurate than remote field testing for ferrous tubes. It is slower, at approximately one inch per second, and needs thorough cleaning and water-filled tubes.
What standards govern tube inspection at TCR?
Eddy current examination of tubular products follows ASTM E243 and ASTM E690, with ASTM E2884 for array probes; remote field testing follows ASTM E2096, and examinations run under ASME Boiler and Pressure Vessel Code Section V. Equipment and technique characterisation follows ISO 15548-1. Tube-by-tube condition maps and remaining-life estimates accompany the reports.
How are tubes prepared for inspection?
All tubes are cleaned before testing by hydro jetting at pressures from 280 to 560 kg/cm2, and cleaning adequacy is verified by passing a dummy probe or rod through each tube. Flaw signals recorded during testing are evaluated against calibration standards by certified eddy current technicians.