
Residual stress measurement by X-ray diffraction (XRD) reads the stress locked into the surface layer of a crystalline part from the change in its lattice spacing, without cutting the part. TCR Engineering, Navi Mumbai, measures residual stress by XRD to ASTM E2860 on welds, machined and shot-peened parts for clients across India, reported outside its NABL and NADCAP scopes.
- What it measures: the magnitude and sign of residual stress, tensile or compressive, in MPa, at each measured point.
- Method: the sin-squared-psi technique of ASTM E2860, reading lattice spacing with the specimen tilted.
- Typical parts: welds and heat-affected zones, machined and ground surfaces, shot-peened and coated parts.
- Accreditation: reported outside NABL certificate NABLT0726MH18640 and outside the NADCAP AC7101 scope.
At TCR, we continue to push the boundaries of materials testing and structural integrity evaluation. In line with our mission to provide solutions to the industries we serve, we are proud to announce the launch of our Residual Stress Measurement by X-Ray Diffraction (XRD), a non-destructive, precision technique performed in compliance with ASTM E2860-20.
Why Measure Residual Stress?
Residual stresses are locked-in stresses within a material even in the absence of external forces or loads. They can arise due to welding, machining, casting, rolling, or heat treatment processes and play a crucial role in:
- Fatigue life
- Crack initiation and propagation
- Corrosion resistance
- Distortion during service
- Dimensional stability of components
Understanding and controlling residual stress is key to ensuring product reliability, especially in high-performance sectors such as aerospace, automotive, energy, petrochemical, defence, and advanced manufacturing.
Our New Capability: X-Ray Diffraction (XRD) for Residual Stress
TCR Engineering's Residual Stress Measurement setup is based on X-ray diffraction (XRD), the industry-standard technique to accurately determine the magnitude and orientation of residual stresses at and near the surface of crystalline materials.
We measure to ASTM E2860-20, the standard practice for residual stress measurement by X-ray diffraction, and report the results outside TCR Engineering's NABL and NADCAP accredited scopes.
How XRD Measures Residual Stress – The Principle Explained
General XRD Peak Principle
When a material is irradiated with X-rays, the crystalline planes diffract the X-rays in specific directions according to Bragg's Law:
nλ = 2d sinθ
- λ is the X-ray wavelength
- d is the interplanar spacing
- θ is the diffraction angle
- n is the order of reflection
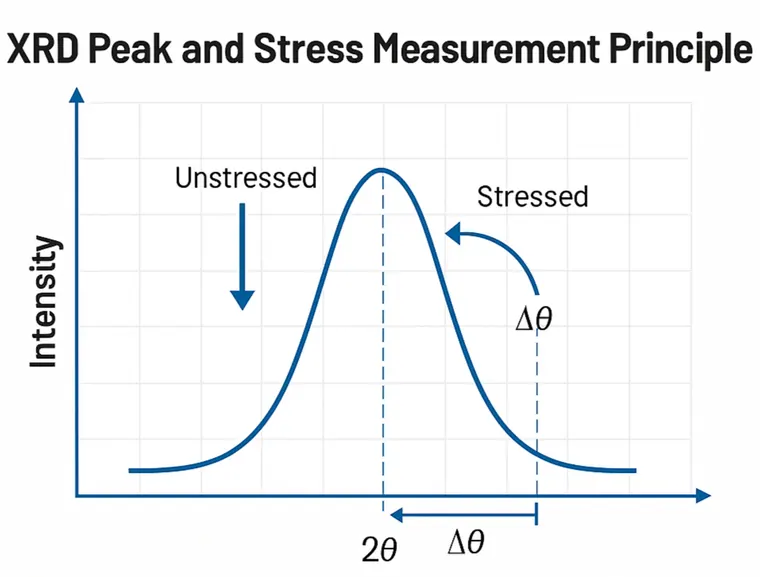
A detector records the diffraction peaks, and their precise position (2θ) reveals the spacing between atomic planes (d-spacing).
Residual Stress Measurement Principle
Stress alters the spacing between atoms. When a material is under stress, the lattice planes expand or contract, causing a measurable shift in the diffraction angle (Δθ).
By measuring this shift at different tilt angles (ψ), the corresponding strain components are calculated. From these strain values, using elastic constants (Young’s modulus and Poisson’s ratio), we determine the residual stress using the fundamental relationship:
σ = E / (1 + ν) * (Δd / d₀)
Where:
- σ = Residual stress
- E = Young’s modulus
- ν = Poisson’s ratio
- Δd = Change in interplanar spacing
- d₀ = Stress-free reference spacing
This process is non-destructive and applicable to a wide range of metallic and ceramic components.
Key Features of TCR’s XRD Residual Stress Measurement
- ✅ Conforms to ASTM E2860-20
- ✅ Non-destructive: Surface or near-surface measurements
- ✅ Point by point: stress read at each measured location
- ✅ Quantitative: Tensile or compressive stress values in MPa
- ✅ Versatile: Suitable for welds, machined parts, coatings, castings, and more
- ✅ On-request stress depth profiling using layer removal or electropolishing
Applications
- Welds and heat-affected zones (HAZ)
- Shot-peened and cold-worked components
- Aerospace turbine blades and engine parts
- Automotive transmission and suspension parts
- Additively manufactured (3D printed) metals
- Coatings and surface treatments
Why Choose TCR?
TCR has carried out metallurgical work since 1973. Our investments in the latest XRD equipment and training help our clients gain deep insights into stress behaviour, critical for product performance, failure prevention, and life prediction.
Let Us Talk Stress – Before It Becomes a Problem!
TCR’s engineers are ready to support your material reliability goals. Whether you are qualifying a new process, investigating a failure, or optimising a product for durability, our Residual Stress Measurement by XRD can give you the confidence to move forward.
FAQ
What does residual stress measurement by XRD tell you?
It gives the magnitude and sign of the residual stress in the surface layer of a crystalline part, tensile or compressive, in MPa, at each measured point. The reading comes from the shift in lattice spacing that stress causes, so the part is measured without being cut or destroyed.
Which standard does TCR Engineering use for residual stress by XRD?
TCR Engineering measures residual stress by X-ray diffraction to ASTM E2860, using the sin-squared-psi technique. ASTM E2860 is not on NABL certificate NABLT0726MH18640 or on the NADCAP AC7101 scope, so results are reported as measurements to the named method, outside the accredited scope.
Which parts can be measured for residual stress by XRD?
Welds and heat-affected zones, machined and ground surfaces, shot-peened and cold-worked components, coatings, castings and additively manufactured metals can all be measured. The method suits crystalline materials, metallic and ceramic, and a stress depth profile can be built on request by removing layers between readings.
Why measure residual stress at all?
Residual stress adds to the service load. Tensile residual stress at a surface drives fatigue crack initiation and stress-corrosion cracking, while a controlled compressive layer, such as one left by shot peening, resists them. Measuring it confirms whether a weld procedure or a peening treatment left the stress state the design assumes.