Services · Materials Testing
Welder Qualification Test and Welding Procedure Qualification (WPS, PQR)
A welder qualification test proves the person; a PQR proves the procedure. Both are welded under witness, tested in one NABL accredited laboratory and recorded with the range qualified.
Request a Quote
In brief
TCR Engineering Services Pvt. Ltd. runs welder qualification tests, WPS review and PQR qualification in Navi Mumbai, India, testing coupons at its NABL ISO/IEC 17025:2017 accredited laboratory (NABLT0726MH18640) to ASME Section IX, AWS D1.1, API 1104, IS 7318 and EN ISO 9606. CSWIP and AWS CWI inspectors witness the tests; an IIW International Welding Specialist endorses the records.
What does a welder qualification test at TCR cover?
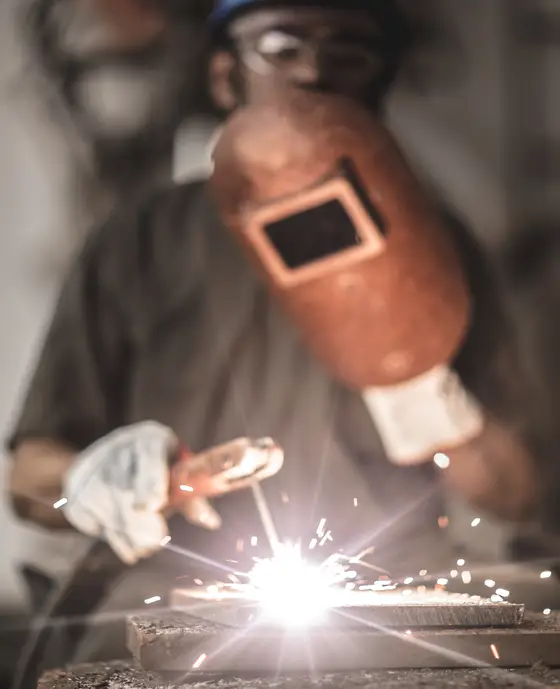
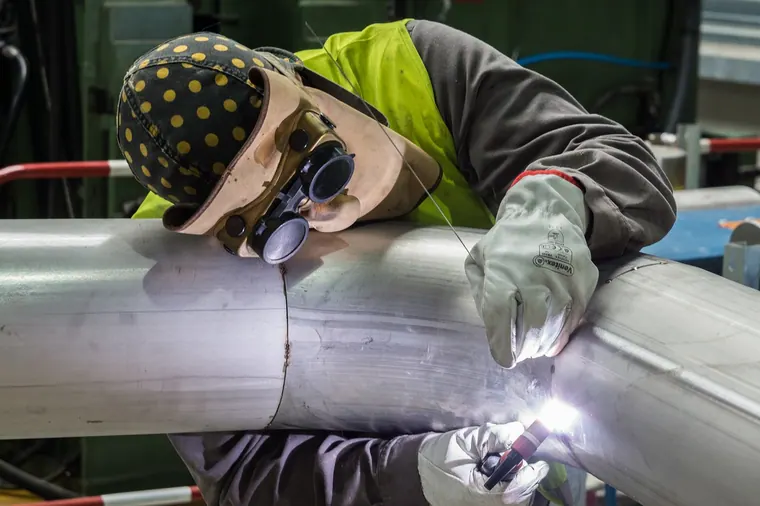
A welder qualification test proves that a welder can deposit sound weld to a qualified WPS; a procedure qualification proves the WPS itself. At TCR Engineering the coupon is welded under witness, tested at the NABL accredited laboratory in Mahape, Navi Mumbai, and recorded with the qualified range, to ASME Section IX, AWS D1.1, API 1104 or IS 7318.
- Witness: CSWIP or AWS CWI certified welding inspectors, each named with the certificate on the record.
- Tests on the coupon: bend, nick break, macro, tensile and radiography, as the governing code names them.
- Record: the welder performance qualification record stating the range qualified, with the test and NDT reports.
- Identity card: issued by TCR in India, and in Saudi Arabia by TCR Arabia, the group's joint venture in Dammam.
- Endorsement: records endorsed by Sachin Ram Bhadange, IIW-certified International Welding Specialist and IIW-certified welding inspector, who leads TCR's welding inspection service.
The capability extends to CTOD on welding electrodes at negative 45 degrees Celsius (E7018, E7018-1) and CTOD per ONGC Spec 2009F Rev. 8 with FMA preparation.
Coverage extends to AWS D1.2 for structural aluminium, ASME Section VIII for pressure-vessel fabrication, and API 1104 for pipeline and cross-country pipework welds, with coupon programmes combining visual, mechanical, metallographic, and non-destructive examination.
TCR Engineering Services' welder certification and welding procedure programme covers:
- Welder Qualification Testing for performance qualification and certification of welders (welder and welding operator performance qualification, WQT) to ASME Sec. IX, ASME Sec. VIII, ANSI, AWS D 1.1, AWS D 1.2, API 1104 etc.
- Preparation of the Welding Procedure Specification (WPS) for the project or the client's requirements
- Coupon Testing as per Welding Procedure Qualification including visual examination, mechanical testing, metallographic examination, and non-destructive testing
- Documentation of the Procedure Qualification Record (PQR) as per ASME Sec. IX, ASME Sec. VIII, ANSI, AWS D1.1, AWS D1.2, API 1104 etc.
- Detailed weld inspection including review of the qualification e.g. weld procedure specification, welder performance qualification, validity for process materials and consumable items, equipment, setup and other factors including certificates of calibration and/or conformity governing the task
- Ascertain safety of operations for self, welder and other workers in the vicinity, particularly ultraviolet radiation from arc during welding
Welding procedure programme on site: the welding inspector deployed on-site by TCR is responsible for monitoring and verifying conformity of tasks against all the relevant requirements including codes, specifications and/or standards:
- Ascertain the weld procedure(s) employed
- Review the weld procedure and welder qualifications
- Supervise weld profile preparation
- Inspect joint fit-up
- Oversee filler metals and consumable materials
- Ensure correct welding parameters are maintained
- Perform visual examination on completion of welding
- Monitor specified preheat and post-weld heat treatment
- Monitor physical examination, including non-destructive, hydrostatic and mechanical tests
- Where required, send test samples to the TCR Engineering Services materials testing laboratory
- Verify that all required visual inspections and non-destructive examinations are completed as specified
Based on the requirements, the inspector carries the measuring aids the checks need:
- Inspection Mirrors
- Torch or other Electrical Lighting Facilities (permitted by safety codes eg. 24V system etc.)
- Physical Size Measuring Instruments such as Welding Gauge, Rule, Vernier etc.
- Electrical Parameter Measuring Instruments such as an Ammeter, Voltmeter etc.
- Temperature Measuring Instruments (Thermometer)/Aids (Thermo Chalk)
In the laboratory, the coupons are tested and the qualification records assembled:
- TCR Engineering's materials testing laboratories in Navi Mumbai and Bhubaneswar undertake mechanical testing and chemical analysis as recommended in ASME Section IX, ASME Section VIII Division-1, AWS D1.1, API 1104 & Customer Specifications. The laboratories also test electrodes for qualification to ASME Section II Part C and IS 814. These tests are done for Welding Procedure Specification (WPS)/ Procedure Qualification Record (PQR), Welder Performance Qualification (WPQ) & Production Weld Coupons.
- The laboratory is NABL accredited to ISO/IEC 17025:2017. Tests done for WPS as per ASME Section IX & API 1104 include All Weld Tensile Test, Transverse Tensile Test (as per API/ISO), Nick Break Test, Bend Test, Macro, Micro, Hardness, Chemical Analysis, Charpy V Notch Impact, and Radiography of weld coupon.
- Coupons required: one coupon on 12” NB pipe; four coupons on 2” NB pipe for API 1104, and four for ASME Section IX.
- TCR Engineering's CSWIP and AWS CWI inspectors provide consultancy as IIW-IWS (RWC-External) for welder training and certification, including training programmes for staff & welders, guidance for preparation of Quality Manual, Procedures, Work Instructions and Witness/Review of WPS/PQR/WPQ tests.
Standards: ASME Section IX 2023 Edition (WPS, PQR, WQT), AWS D1.1 2025 Edition (structural steel), AWS D1.2 (structural aluminium), AWS D1.5 (bridge welding), API 1104 22nd Edition (2021) (pipeline welds), IS 7318 (welder qualification), EN ISO 9606 series.
Inspecting the Welds on the Job
Testing a coupon proves a procedure or a welder; it does not prove the production weld. The inspection of the welds themselves, from fit-up to final visual, together with WPS preparation and review, witnessing of the qualification tests and endorsement of the records by an IIW-certified International Welding Specialist, is set out on welding inspection.
- Before the coupon: the WPS written or reviewed against the code, and the qualification type and filler checked against the heat treatment the joint can take.
- During production: fit-up, preheat, welding parameters, interpass temperature and the run sequence inspected against the qualified WPS.
- After welding: final visual examination, PWHT records and the NDT the code calls for, with samples sent to this laboratory where a test is needed.
Welder Testing Agency Work, From Witness to Certificate
A fabricator that appoints a welder testing agency buys one chain: the test witnessed by a certified inspector, the coupons in the agency's custody to an ISO/IEC 17025 laboratory, radiography and mechanical tests signed by qualified personnel, and the certificates returned with the coupons. TCR runs every link, from Mahape in India and, in Saudi Arabia, through TCR Arabia.
| Link in the chain | What the scope of work asks for | How TCR covers it |
|---|---|---|
| Witness | The welder test witnessed by a certified welding inspector, for example CSWIP 3.1 or 3.2, or AWS CWI | Witnessed by CSWIP or AWS CWI certified welding inspectors, each named with the certificate on the record, and in the Kingdom by Saudi Aramco approved inspectors engaged by TCR Arabia on contract; see welding inspection |
| Coupon custody | Coupons collected from the fabricator's site, held securely after testing and returned | Collection from site, the holding period after testing and the return to site are agreed in writing in the offer |
| Radiography | Each coupon radiographed by a Level II technician, the films interpreted by a qualified film interpreter and the report endorsed at Level III | ASNT RT Level II technicians, RTFI-qualified film interpreters and ASNT Level III radiography personnel on the group's radiography bench; TCR Arabia is Saudi Aramco approved for conventional NDT including RT (notified 1 September 2021) |
| Mechanical tests | Bend, macro and nick break, and the other tests the code names | Bend, macro and nick break to ASME Section IX and API 1104 at the Mahape laboratory, NABL accredited to ISO/IEC 17025:2017; in the Kingdom, at TCR Arabia's IAS accredited laboratory in Dammam, on Saudi Aramco's list of approved in-Kingdom laboratories for welding procedure qualification testing (effective 22 June 2020) |
| Certificates | The welder certificate, and the identity or job clearance card the owner's system uses | The welder performance qualification record stating the range qualified, with the test and NDT reports, and a welder identity card, issued by TCR in India and by TCR Arabia in the Kingdom; any job clearance card format the owner specifies is agreed in the offer |
| Quality dossier | Calibration certificates, quality plan, inspection and test plan, HSE procedures and the quality organisation chart | Calibration certificates for every test machine and instrument used, traceable under ISO/IEC 17025; the plans, procedures and organisation chart submitted for the client's approval before work starts |
For Saudi Aramco work the agency is TCR Arabia, the joint venture in Dammam, which Saudi Aramco's Inspection Department approved as a Welder Testing Agency for qualifying welders working for Saudi Aramco (vendor 10040677, notified 20 July 2020). Its approvals are listed on TCR Arabia; where a contract names an owner's approval, its current status is confirmed in writing with the offer.
Documents
Download the reference documents for this page. Every file is hosted on this domain and is also listed in the site document library.
Related insights
5 published insights on this site bear directly on Welder Qualification. They are below; the full index carries all 166 Materials Testing insights.
-
Rebuilding a 13Cr valve seat on a WCB body: the qualification is an overlay, and E410 is the wrong filler
A request for a WPS to rebuild scored 13Cr gate valve seats looks routine. It is two decisions most repair shops get wrong: the build-up is qualified…
-
Why Welder Qualification Testing Services Mumbai Are Make-or-Break for Your Projects
Welder qualification testing services Mumbai ensure project success. ASME, API standards compliance. Choose certified professionals for quality.
-
Weld and Braze Inspections Across India
Expert weld & braze inspections across India, with ASME IX-certified methods for defence & industrial components. Trusted by top sectors.
-
Welding Consultancy, Welders Training & Qualification
TCR Engineering delivers expert welding consultancy, training, and quality control to ensure defect-free, high-integrity fabrication.
-
Welding Certification and Welder Qualification Services from TCR
Comprehensive welder certification and welding procedure qualification programme.
Frequently asked questions
Which codes govern welder and procedure qualification at TCR?
Welder qualification and procedure qualification run to ASME Section IX, AWS D1.1 for structural steel, AWS D1.2 for structural aluminium, AWS D1.5 for bridge welding, API 1104 for pipeline welds, IS 7318 for Indian standard qualification, and the EN ISO 9606 series, with CSWIP and AWS CWI certified personnel witnessing.
What testing does a PQR coupon programme include?
Coupon testing for WPS and PQR per ASME Section IX and API 1104 includes all-weld tensile, transverse tensile, nick break, bend tests, macro and micro examination, hardness, chemical analysis, Charpy V-notch impact, and radiography of the weld coupon, combining mechanical, metallographic, and non-destructive examination in one laboratory programme.
Can TCR qualify welding electrodes as well as welders?
Yes. Electrode qualification runs per ASME Section II Part C and IS 814 in the same laboratories, for Welding Procedure Specification, Procedure Qualification Record, Welder Performance Qualification, and production weld coupons, so consumable qualification and welder qualification can run as one programme with common documentation.
What does TCR's on-site welding inspector cover?
The deployed inspector reviews weld procedures and welder qualifications, supervises weld profile preparation and joint fit-up, oversees filler metals and consumables, verifies welding parameters, monitors pre and post weld heat treatment, and performs visual examination on completion, with test samples routed to the materials testing laboratory where required.
Can TCR act as the welder testing agency for a project in Saudi Arabia?
Yes, through TCR Arabia, the group's joint venture in Dammam. Saudi Aramco's Inspection Department approved TCR Arabia as a Welder Testing Agency for qualifying welders working for Saudi Aramco (vendor 10040677, notified 20 July 2020), and its IAS accredited laboratory runs bend, nick break and macro tests to API 1104 and ASME Section IX. TCR Arabia issues the welder qualification records and welder identity cards.
What is the difference between a welder qualification test and a welding procedure qualification?
A welding procedure qualification proves the procedure: a PQR coupon is welded to a draft WPS and tested, and the qualified WPS then governs production. A welder qualification test proves the person: the welder deposits a coupon to that WPS, and the record states the positions, thicknesses and processes the welder is qualified to weld.
Who issues the welder qualification certificate and identity card?
TCR Engineering issues the welder performance qualification record, with its test and NDT reports, and a welder identity card for work in India; TCR Arabia, the group's joint venture in Dammam, issues them in Saudi Arabia. Records are endorsed by Sachin Ram Bhadange, an IIW-certified International Welding Specialist and IIW-certified welding inspector.