
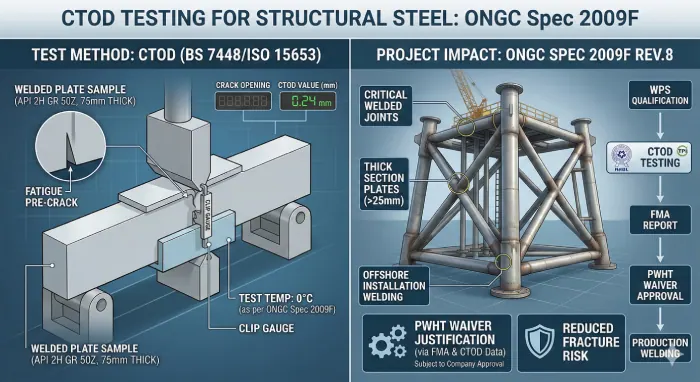
A CTOD test for structural steel measures how far a sharp crack in a weld, heat-affected zone or plate opens before it extends. Under ONGC Specification 2009F Rev. 8 the welding procedure must reach at least 0.20 mm at 0 °C; TCR Engineering tests it at its NABL-accredited Mahape laboratory, Navi Mumbai, to BS 7448, ISO 15653 and ISO 12135.
- Minimums at 0 °C: WPS 0.20 mm, welding consumable 0.25 mm, material 0.35 mm
- At least three valid specimens per set
- The Fracture Mechanics Assessment behind a PWHT waiver is an Engineering Critical Assessment prepared by TCR Advanced Engineering
- Background: why a CTOD test is required, and the CTOD test for welding electrodes
CTOD testing for structural steel is a critical and often misunderstood requirement in Indian heavy engineering and offshore fabrication projects. When a project involves thick-section welded plates, high-strength steels, or critical structural joints, the question of fracture toughness is not optional. It is a code requirement, a safety obligation, and increasingly, a procurement checkpoint that decides whether a fabricator can commence welding at all.
This article breaks down what CTOD testing actually involves, why it matters for Indian infrastructure and offshore projects, what the ONGC specification requires, and how experienced testing firms approach it.
What Is CTOD Testing and Why Does It Matter?
Crack Tip Opening Displacement (CTOD) is a fracture mechanics test that measures a material's resistance to crack extension under load. In simpler terms, it answers one question: at what point does a pre-existing crack or flaw in a weld or base metal start to grow in an uncontrolled way?
This matters enormously in structural applications, especially when:
- Thick steel plates are used in welded assemblies
- The structure will operate in low temperatures or cyclically loaded conditions
- The welding process introduces residual stresses or HAZ (Heat Affected Zone) brittleness
- The material grade is a high-strength steel such as API 2H Grade 50Z or equivalent
A structure can pass visual inspection, radiography, and even standard mechanical tests and still fail catastrophically under fracture conditions if the fracture toughness of the weld or HAZ is inadequate. CTOD testing closes that gap.
How CTOD Testing Fits Into Indian Engineering Projects
In India, CTOD testing is most commonly required in:
- Offshore platform fabrication for ONGC and other oil and gas clients
- Subsea pipeline and riser fabrication
- Heavy structural steel fabrication where thick sections are involved
- Pressure vessel and piping systems in sour or critical service
- Pre-qualification of welding procedures (WPS/PQR) under ASME, AWS, DNV, and ONGC standards
The governing documents typically referenced include ONGC Functional Specification 2009F Rev.8, BS 7448, ISO 15653, ISO 12135, and BS 7910. Each of these specifies how the test is to be conducted, what values must be achieved, and under what conditions.
What ONGC Specification 2009F Rev.8 Actually Requires
For structural welding, Clause ST 3.3 of ONGC Spec 2009F Rev.8 outlines the weld procedure qualification requirements. Within this, CTOD testing is addressed in detail under the fracture mechanics provisions.
The key requirement: the minimum CTOD value shall be 0.20 mm when tested at 0°C.
This applies to full penetration test welds representing the maximum thickness of materials to be welded. The specification further requires:
- A minimum of three valid CTOD specimens per test set
- Separate tests for single-sided and double-sided weld preparations
- The steel selected for testing must have a minimum Carbon Equivalent (CE) no more than 0.02 below the maximum CE value to be used in production
- Test plates must be welded using heat inputs representative of the highest to be used in production
Under Clause ST 3.5.10, CTOD testing is directly linked to Post Weld Heat Treatment (PWHT) requirements. When welding takes place during the installation phase offshore and PWHT cannot be carried out, CTOD testing combined with a Fracture Mechanics Assessment (FMA) as per BS 7448/ISO 15653 can be used to justify waiving the PWHT requirement, subject to written approval from the Company.
This is a critical technical provision. In practice, it means that CTOD testing is not just a quality check. It is often the engineering justification that allows offshore welding to proceed without PWHT, which would otherwise be impractical or impossible.
Clause QA 1.3.13 further specifies that:
- Material CTOD value must meet or exceed 0.35 mm
- Welding consumable CTOD value must meet or exceed 0.25 mm
- WPS CTOD value must meet or exceed 0.20 mm
- Testing must be carried out from Government-accredited or NABL-accredited laboratories with prior information to ONGC
What a CTOD Test Establishes for ONGC Qualification
Engineers and procurement heads read a CTOD report for a small set of decisions, and each one is visible on the report itself.
- The critical CTOD value of each specimen, as δc, δu or δm, with its load versus crack opening record; the ONGC acceptance applies to the least value
- The test temperature, 0 °C for ONGC structural qualification, and the specimen geometry, B × 2B SENB or square-section B × B
- Whether the fatigue crack tip sat in the intended zone (weld centreline, fusion line or heat-affected zone), confirmed by post-test metallography
- The data a Fracture Mechanics Assessment to BS 7910 uses where a PWHT waiver is sought; that assessment is prepared by TCR Advanced Engineering
CTOD Testing for API 2H Grade 50Z at 75 mm Thickness: Specific Considerations
API 2H Grade 50Z is a notch-tough carbon-manganese plate steel developed specifically for offshore structural applications. The Z suffix indicates through-thickness ductility requirements, making it particularly suited for T-joints and node connections in offshore platforms.
At 75 mm thickness, certain testing parameters deserve attention:
Specimen Size: TCR tests fracture toughness specimens from 7.5 mm to 90 mm thick, so a 75 mm plate is tested at full thickness as a square-section B × B specimen, the geometry TCR uses from 75 mm to 90 mm. Where the standard B × 2B specimen is preferred and cannot be machined from the available plate without losing traceability to the required microstructural zone, the chosen geometry is documented on the report and confirmed as within the laboratory's accredited capability.
Notch Positioning: At this thickness, multiple notch positions (weld centreline, fusion line and set distances into the heat-affected zone) are typically tested to fully characterise the weld quality across all zones, consistent with AWS D1.1 and the ONGC specification requirements.
Heat Input Sensitivity: For thick structural plates, the cooling rate during welding strongly influences HAZ microstructure. The WPS qualified for this thickness must specify heat input tolerances carefully, and the CTOD specimens must be welded using the upper bound of this heat input range.
CE Value Tracking: The test plate CE must be within 0.02 of the maximum production CE. This must be verified from the material test certificate before test plate welding begins.
Common Mistakes Engineering Teams Make With CTOD Testing
TCR Engineering's Technical Head, Avinash Tambewagh, has observed a consistent pattern in how CTOD testing requirements are handled on Indian fabrication projects.
"The most common issue we encounter is that CTOD testing is treated as a last-minute compliance step rather than being planned into the WPS qualification programme from the beginning. By the time teams realise the specimen extraction orientation is wrong, or that their test plate was welded at the wrong heat input, fabrication schedules have already been compromised. The test itself is straightforward. What requires careful thinking is the preparation."
Beyond poor planning, other frequent issues include:
- Using previously qualified PQRs without checking CTOD data validity. ONGC Spec 2009F Rev.8 explicitly disallows previously qualified procedures for CRA and offshore structural applications. CTOD data from an old PQR on a different project or plate thickness is not transferable.
- Ignoring post-test metallography. Skipping metallographic verification of crack tip position, especially for HAZ specimens, can make test results invalid on scrutiny. A test report without this is incomplete under strict interpretation of the standard.
- Specimen notch position errors. For fusion line specimens, even a small deviation in notch position relative to the fusion line can place the crack tip in the weld metal rather than the HAZ. This changes the result entirely.
- Inadequate temperature control during testing. Reaching and holding 0°C uniformly through the specimen cross-section at 75 mm thickness requires a properly calibrated temperature conditioning bath and careful soak time. Shortcutting this step produces unreliable data.
- Misidentifying the controlling standard. BS 7448, ISO 15653, and ISO 12135 have differences in specimen preparation and calculation methods. The applicable document depends on the project specification and must be confirmed before testing begins.
The Role of Fracture Mechanics Assessment in Structural Projects
A Fracture Mechanics Assessment (FMA) is a document that uses CTOD or K₁c data to demonstrate that a structure containing known or assumed flaws of a given size will not fail by fracture under the applied loads and environmental conditions.
In the context of ONGC offshore structural projects, the FMA serves a specific regulatory purpose: it is the engineering basis for waiving PWHT under Clause ST 3.5.10.
The FMA must be prepared in accordance with BS 7910 and must include:
- The applied stress state at the weld joint (including residual stresses)
- The assumed flaw size, typically based on the NDT detection limit
- The fracture toughness data from CTOD testing
- A demonstration that the largest undetectable flaw will not cause fracture at the design load
The FMA report is submitted to the Company (ONGC) for review and approval before production welding commences. It is a project-specific document and cannot be transferred between projects or material grades.
Accreditation and Standards: What to Confirm Before Selecting a Testing Laboratory
For ONGC-governed projects, the specification is clear. CTOD testing must be performed at Government-accredited or NABL-accredited laboratories.
When evaluating a testing partner, the following should be confirmed:
- NABL accreditation scope specifically covering fracture toughness testing per BS 7448, ISO 15653, or ISO 12135
- Equipment capacity for the specimen dimensions involved (at 75 mm thickness, the machine load capacity and fixture dimensions must accommodate the specimen geometry)
- Temperature conditioning capability below the 0 °C test temperature, with margin
- Availability of an appropriate COD gauge with the correct gauge length for the specimen
- Experience with offshore or ONGC-governed projects and familiarity with the specific documentation requirements, including FMA preparation
TCR Engineering's NABL-accredited Mahape laboratory (certificate NABLT0726MH18640) carries out CTOD testing under ONGC Specification 2009F Rev.8 for offshore structural projects, including thick-section API 2H Grade 50Z plate applications; the Fracture Mechanics Assessment is prepared by TCR Advanced Engineering.
How CTOD Testing Connects to NDT and the Broader QA Programme
CTOD testing does not exist in isolation. It sits within a broader quality assurance framework that includes:
- WPS and PQR development incorporating all mechanical testing including CTOD, Charpy, hardness traverses, and tensile tests
- NDT coverage per ONGC Spec 2009F (full UT and MPI coverage for major brace to chord joints, and PAUT or TOFD for thicker structural joints)
- ITP (Inspection and Test Plan) submission and approval before fabrication commences
- Third-party inspection (TPI) witnessing of WPS qualification testing, including CTOD
- Production records maintained throughout fabrication, with CTOD test certificates as mandatory supporting documents
The CTOD result defines the acceptance threshold for defects under the fracture mechanics framework. The NDT system must then be capable of detecting flaws larger than this threshold. These two systems must be engineered together, not independently.
Conclusion
CTOD testing for structural steel is a technically demanding but non-negotiable part of welding procedure qualification for any serious offshore or heavy industrial project in India. Understanding the requirements of ONGC Specification 2009F Rev.8, selecting a properly accredited laboratory, planning specimen geometry and notch positions correctly, and integrating CTOD data into the broader NDT and QA programme are the factors that determine whether a project passes or fails at the qualification stage.
TCR Engineering covers test planning, specimen preparation and CTOD testing for ONGC-governed structural projects, and TCR Advanced Engineering prepares the Fracture Mechanics Assessment report. For engineering teams that want their CTOD programme structured correctly from the start, the specimen geometry, notch positions and test temperature are best agreed before the test plates are welded.
Frequently Asked Questions
What is CTOD testing and when is it required?
CTOD (Crack Tip Opening Displacement) testing is a fracture toughness test that measures how resistant a material or weld is to crack growth. It is required during welding procedure qualification for thick structural sections, offshore platform fabrication, critical piping systems, and any application governed by ONGC Spec 2009F Rev.8 or similar standards such as BS 7448, ISO 15653, and DNV-OS-F101.
What CTOD value is required under ONGC Spec 2009F Rev.8?
The WPS (welding procedure) must achieve a minimum CTOD value of 0.20 mm at 0°C. The base material must achieve 0.35 mm and the welding consumable must achieve 0.25 mm. These are minimum values and any specimen falling below the limit causes the qualification to fail.
Can a previously qualified PQR be used to meet CTOD requirements for a new project?
For standard carbon steel piping in some service categories, previously qualified WPQTs may be accepted under ONGC Spec 2009F Rev.8 subject to conditions. However, for CRA materials, offshore structural applications, and situations involving PWHT waiver, fresh project-specific CTOD testing is mandatory.
What is a Fracture Mechanics Assessment (FMA) and why is it needed?
An FMA is an engineering document that uses CTOD test data to demonstrate that the structure is safe in the presence of the largest flaw that might escape detection by NDT. Under ONGC Spec 2009F Rev.8, an FMA prepared per BS 7910 can be used to justify waiving PWHT for offshore installation welding, subject to Company approval.
How many CTOD specimens are required per test?
A minimum of three valid specimens per test set are required under ONGC Spec 2009F Rev.8 and BS 7448/ISO 15653. All three specimens from the set must individually meet the minimum CTOD value requirement.
What is the difference between δc, δu, and δm in a CTOD test report?
These represent different fracture events observed during testing. δc is the CTOD at unstable fracture without prior ductile tearing. δu is the CTOD at unstable fracture with prior ductile tearing. δm is the CTOD at maximum load without fracture instability. The governing acceptance criterion in the ONGC specification applies to the least value measured.
Does specimen thickness affect CTOD test results?
Yes. Standard specimens are B × 2B in cross-section. At 75 mm plate thickness, TCR tests at full thickness, using a square-section B × B specimen, which it runs from 75 mm to 90 mm; its fracture toughness range is 7.5 mm to 90 mm thick. The specimen geometry is documented on the report and confirmed as within the laboratory's accredited scope.
Which laboratory accreditation is acceptable for CTOD testing under ONGC specifications?
ONGC requires testing at Government laboratories, Government-accredited laboratories, or NABL-accredited laboratories. The accreditation scope must specifically cover fracture toughness testing under the applicable standard. This must be confirmed before engaging a laboratory.
Who prepares the Fracture Mechanics Assessment for an ONGC PWHT waiver?
The Fracture Mechanics Assessment that uses CTOD results to support a PWHT waiver under ONGC Specification 2009F is prepared and signed by TCR Advanced Engineering, a group company of TCR Engineering. TCR Engineering's Mahape laboratory carries out the CTOD testing under its own NABL accreditation, and the Company's written approval is still required.
At what temperature is CTOD tested under ONGC Spec 2009F?
ONGC Specification 2009F Rev. 8 sets its CTOD minimums at 0 °C for structural welding procedure qualification. TCR Engineering tests at 0 °C, at room temperature or at other sub-zero temperatures down to -65 °C in either of its two cold chambers, as the specification and the minimum design temperature require.