
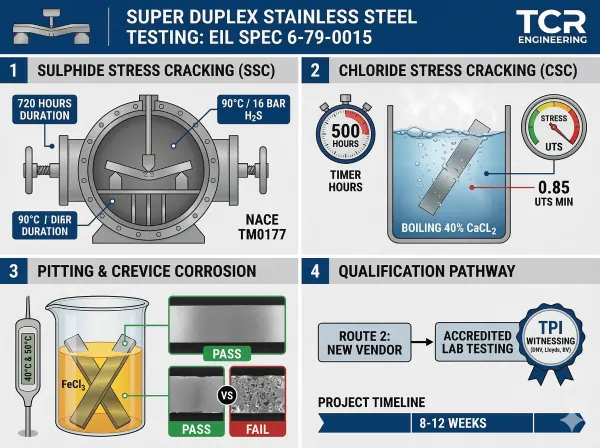
TCR Engineering tests super duplex stainless steel (SDSS) to EIL specification 6-79-0015 at its Mahape laboratory in Navi Mumbai, India: sulphide stress cracking to NACE TM0177 and ASTM G39, chloride stress corrosion cracking to ASTM G36, and pitting and crevice corrosion to ASTM G48 Methods A and B. Each of these standards is on NABL certificate NABLT0726MH18640.
- Sulphide stress cracking: NACE TM0177 and ASTM G39, two conditions of 720 hours each
- Chloride stress corrosion cracking: ASTM G36
- Pitting and crevice corrosion: ASTM G48 Methods A and B
- Ferrite content to ASTM E562 and detrimental intermetallic phases to ASTM A923
- Witnessing: by a TPI agency that EIL or the purchaser accepts
Super duplex stainless steel testing is one of the most technically demanding qualification processes in the Indian chemical process and oil and gas industry. If you are a procurement head, QA/QC engineer, or project consultant working with EIL-specified materials, chances are you have already encountered the complexity of getting SDSS pipes qualified before they reach the shop floor.
This article breaks down what the pre-qualification process actually involves, why it matters, and what separates a reliable testing partner from one that simply issues a report.

Why Super Duplex Stainless Steel Demands a Higher Level of Scrutiny
Super Duplex Stainless Steel (SDSS), typically conforming to UNS S32750 or UNS S32760, is chosen for aggressive environments, sour gas service, and chloride-containing process streams. It offers a significantly higher Pitting Resistance Equivalent Number (PREN) than standard duplex grades, with EIL's specification 6-79-0015 Rev.3 requiring a PREN above 40.
But a high PREN on paper does not automatically mean the material will survive in service. The microstructure must be right. The ferrite-austenite balance must fall within 35 to 60 per cent. And most critically, the material must pass a rigorous battery of corrosion tests before it is accepted for use.
Procurement teams often underestimate this. A common mistake is treating SDSS qualification as a documentation exercise. It is not. It is a live, time-intensive laboratory process whose length depends on the test matrix, with the completion date confirmed in the quotation.
What EIL Specification 6-79-0015 Rev.3 Actually Requires
Engineers India Limited's standard specification for DSS and SDSS sets out two qualification routes:
Route 1: Vendors with proven track record: Suppliers who have previously supplied SDSS materials to major operators or on EIL-governed projects, with TPI-witnessed test certificates, are considered pre-qualified. They do not need to repeat the full corrosion test matrix.
Route 2: New vendors without track record: If the manufacturer or mill has no such history, a full set of corrosion and mechanical tests must be conducted and witnessed by a third-party inspection agency that EIL accepts for the project.
For most European or international pipe manufacturers entering an Indian EIL project for the first time, Route 2 applies by default.
The Four Corrosion Tests That Cannot Be Skipped
For SDSS materials intended for sour service and chloride environments, all four of the following corrosion tests are mandatory under the specification. TCR Engineering's dedicated corrosion detection and testing laboratory is equipped to run all four; each of the four standards is on its NABL scope, and any condition a specification adds that the scope does not carry is reported outside the NABL scope.
1. Sulphide Stress Cracking (SSC) Test: NACE TM0177 / ASTM G-39
Two test conditions are required for SDSS:
- Condition (i): 24°C, stress at 425 N/mm², test duration 720 hours, using NACE TM0177 solution
- Condition (ii): 90°C, stress at 390 N/mm², partial pressure of H₂S at 16 bars, duration 720 hours
The acceptance criterion is that the sample must not fail before 720 hours. A minimum of three specimens per condition is required by the standard.
This is a long-duration test. The 720-hour window alone means nearly a month of continuous exposure in a controlled autoclave environment. Any team quoting a schedule shorter than the exposure itself for SSC at elevated temperature and pressure is either not following the standard or is misrepresenting the scope.
2. Chloride Stress Cracking (CSC) Test: ASTM G-36
Specimens are exposed to boiling 40% calcium chloride solution at 100°C with pH maintained around 6.5. The test runs for 500 hours. The acceptance criterion is that the stress required to cause rupture must exceed 0.85 times the minimum specified ultimate tensile strength of the material.
3. Pitting Corrosion Test: ASTM G48 Method A
For SDSS, specimens are immersed in 6% ferric chloride solution at 40°C and again at 50°C, for 24 hours each. No pitting is permitted on the surface at 40°C. At 50°C, weight loss is reported to the client for review.
4. Crevice Corrosion Test: ASTM G48 Method B
Similar ferric chloride solution is used, but the test is conducted at 30°C for 24 hours. No crevice formation is acceptable at this temperature.
What Manoj Prabhakar Singh Says About Common Testing Errors
Manoj Prabhakar Singh, Department Head, Corrosion Testing at TCR Engineering, has worked on pre-qualification programmes for EIL, SABIC, and Aramco-specified duplex and super duplex materials across multiple Indian and Middle East refinery projects.
"The biggest issue we see is that clients send us samples without confirming the correct specimen geometry upfront. For the four-point bend SSC test, the fixture dimensions, the specimen length, and the stress application method must all match exactly what the standard prescribes. A 5mm variation in specimen thickness changes the stress distribution significantly. We always verify sample geometry against the specification before machining begins," says Manoj Singh.
This attention to detail at the sample preparation stage is what separates meaningful pre-qualification results from those that fail during client review or TPI witnessing. TCR's mechanical testing capabilities and corrosion division work in close coordination so that specimens are correctly prepared and documented before any test begins.
The Role of Third-Party Inspection in EIL Pre-Qualification
A detail that frequently catches procurement teams off-guard: Under Route 2, the specification requires all corrosion and mechanical tests to be witnessed by an approved TPI agency. The lab report alone is not sufficient. The TPI must witness the tests, and the final test certificate carries both the laboratory report and the TPI endorsement.
The purchase order or EIL names the agencies accepted for the project.
This has a direct impact on project planning. If the TPI agency needs to mobilise to the lab, schedules their witnessing visits separately, and requires multiple visits for different test stages, the total project timeline grows accordingly. For a full EIL SDSS pre-qualification programme, several TPI visits are normal, and the number depends on the scope.
TCR Engineering's third-party inspection team regularly coordinates with approved TPI agencies on behalf of clients, helping manage witnessing schedules so that tests and inspections proceed without unnecessary hold points.
Clients should confirm the number of required TPI visits and their scheduling before issuing a purchase order. This avoids last-minute delays when a downstream contractor is waiting for approved test certificates to proceed with fabrication.
Sample Requirements and What to Send
For SDSS welded pipes to ASTM A928, Grade UNS S32750, the typical sample requirement for a full EIL 6-79-0015 pre-qualification matrix is:
- Pipe sample: OD 219.1 mm x 3.76 mm wall thickness, approximately 250 mm in length
- The laboratory will cut and machine specimens for each individual test from this parent sample
- All specimens must carry the same heat number as the production batch, as the specification requires
For international shipments, the dispatch note and shipping invoice must clearly state that materials are being sent for testing purposes only and carry no commercial value. The receiving laboratory typically handles customs coordination.
You can download TCR Engineering's standard sample size requirements guide before dispatching your samples.
How TCR Engineering Approaches EIL SDSS Pre-Qualification
TCR Engineering's corrosion testing laboratory in Navi Mumbai is equipped with custom autoclaves for sour gas simulation, controlled temperature chambers for high-pressure SSC testing, and a dedicated corrosion team for NACE MR0175/ISO 15156 qualification testing.
The laboratory is accredited by NABL to ISO/IEC 17025:2017 (certificate NABLT0726MH18640). It also evaluates elastomeric materials for sour gas environments, which reflects the same testing rigour demanded by SDSS pre-qualification programmes.
TCR's approach for EIL-governed pre-qualification work includes:
- Pre-test review of the specification clauses applicable to the material grade and service environment
- Confirming sample geometry and machining requirements before cutting begins
- Coordinating TPI witnessing schedules in advance to avoid mid-test delays
- Issuing separate accredited and non-accredited reports in line with NABL guidelines, where applicable
- Providing combined chemical analysis, mechanical testing, and corrosion testing at the same Mahape laboratory, reducing sample transit time and chain-of-custody risk
"When a European manufacturer sends us SDSS pipe samples for EIL qualification, the first thing we do is map every clause of the spec against the service environment declared in the datasheet. If the pipes are going into a sour and chloride environment, all four corrosion tests apply with no exceptions. We set that timeline upfront so there are no surprises later," adds Manoj Singh.
Welding Qualification for SDSS: A Connected Requirement
Pre-qualification of the base material under EIL 6-79-0015 is often followed by, or concurrent with, welding procedure qualification under EIL 6-79-0016. This specification covers consumable qualification, procedure qualification tests (PQT), and welder qualification for DSS and SDSS weldments.
The corrosion test matrix for weld qualification mirrors that of the base material qualification: SSC, CSC, pitting, and crevice corrosion tests are all mandatory for weldments intended for sour and chloride service.
TCR Engineering also supports metallurgy evaluation of weld metal and heat-affected zones, including ferrite content measurement by metallographic method per ASTM E 562, and detection of detrimental intermetallic phases per ASTM A 923. These are mandatory checks under both specifications.
SDSS fabrication areas must also be physically separated from carbon steel and low-alloy fabrication zones. Purge gas oxygen levels must remain below 10 ppm during pipe butt welds to protect corrosion resistance. These are not advisory notes; they are specification requirements.
Clients who plan to weld SDSS components on-site or at a fabrication yard should confirm early whether their welding contractor has an approved WPS/PQR for the specific UNS grade, or whether a full welding procedure qualification programme is also needed.
Beyond Corrosion Testing: The Broader Material Qualification Picture
A complete SDSS qualification programme under EIL 6-79-0015 also includes mechanical testing for tensile strength, yield strength, elongation, and Charpy impact energy at both 20°C and -30°C. These mechanical property checks must be conducted per ASTM A 370 and must meet the minimum values specified for the relevant UNS grade.
For SDSS castings, radiographic inspection per ASME Section V and wet fluorescent penetrant testing per ASME B16.34 are additional mandatory requirements of the specification. TCR's advanced NDT capabilities and conventional NDT services cover both requirements.
For projects where pipeline integrity and long-term asset performance are concerns beyond the immediate pre-qualification scope, TCR Advanced Engineering, the group's asset integrity consulting company, provides Fitness-for-Service assessments, Remaining Life Assessment, and failure and root cause analysis for SDSS and other high-alloy components in service.
Key Timelines to Plan Around
Anyone managing a project schedule that includes EIL SDSS pre-qualification should account for the following:
- SSC test at 90°C/16 bar H₂S: 720 hours (30 days) minimum in the autoclave, plus preparation and reporting time
- CSC test at 100°C: 500 hours (approximately 21 days)
- Pitting and crevice tests: 24 hours per test condition, relatively fast
- TPI coordination and witnessing: adds scheduling lead time at multiple points
- Report review by EIL/client: follows final test completion, on the reviewer's own timeline
In total, the schedule for an SDSS pre-qualification programme under EIL 6-79-0015, from sample receipt to final approved test package, is confirmed in the quotation, assuming no failures that require re-testing.
To get started or discuss your pre-qualification programme with the TCR Engineering team, contact us here or write to sales@tcreng.com.
For further reading on related topics, explore TCR's insights on CTOD testing for welding electrodes and boiler tube failure analysis, or browse the full materials testing blog category.
FAQ: Super Duplex Stainless Steel Testing as per EIL Specification
What is EIL specification 6-79-0015 and when does it apply?
EIL 6-79-0015 is Engineers India Limited's standard specification for Duplex and Super Duplex Stainless Steel. It applies when DSS or SDSS materials are used in sour service or chloride-containing environments on EIL-governed projects. It covers chemical composition, heat treatment, mechanical properties, microstructure requirements, pre-qualification criteria, and corrosion testing.
Is a vendor with a track record exempt from corrosion testing under EIL 6-79-0015?
Yes, partially. Vendors with a documented record of supplying SDSS to major operators or on EIL-governed projects, with TPI-witnessed test certificates, are treated as pre-qualified under the specification. They do not need to repeat the full corrosion test matrix for a new project.
Which TPI agencies are acceptable for EIL SDSS pre-qualification testing?
The tests must be witnessed and endorsed by a third-party inspection agency that EIL or the purchaser accepts for the project, and the purchase order names the accepted agencies. The laboratory report alone is not sufficient.
How many specimens are required for the SSC test as per EIL 6-79-0015?
A minimum of three specimens per test condition is required for the four-point bend SSC test, as the standard mandates triplicate testing for statistically valid results.
Can SSC results from a previous project be reused for a new EIL project?
For base material pre-qualification, previously certified results from the same heat, endorsed by an approved TPI, may be submitted for EIL's review. EIL's decision on acceptance is final. For welding procedure qualification under 6-79-0016, previous test reports are explicitly not recognised for a new job.
How long does EIL SDSS pre-qualification testing take?
For a full corrosion test matrix including SSC at 90°C, the minimum laboratory time is around 30 days just for the sour service SSC test. TPI coordination and report preparation sit on top of that, and the end-to-end schedule to a final approved test package is confirmed in the quotation.
Does TCR Engineering handle international sample submissions for SDSS testing?
Yes. TCR Engineering accepts international sample shipments at its Navi Mumbai laboratory. The shipping invoice must declare the materials as having no commercial value and being sent for testing purposes only. Customs clearance support is available. Contact TCR for shipment instructions.
What happens if SDSS pipe samples fail the pitting corrosion test?
A failure in the pitting corrosion test means the material does not meet EIL pre-qualification criteria for that grade. The manufacturer would need to investigate the root cause, typically related to microstructure, heat treatment, or ferrite-austenite balance, and resubmit samples from a corrected heat. TCR's failure analysis and engineering advisory team can support root cause investigation if required.
Which super duplex stainless steel tests are on the NABL scope at TCR Engineering?
The standards behind the EIL 6-79-0015 corrosion matrix are on NABL certificate NABLT0726MH18640 at Mahape: NACE TM0177 and ASTM G39 for sulphide stress cracking, ASTM G36 for chloride stress corrosion cracking, ASTM G48 Methods A and B, ASTM E562 ferrite content and ASTM A923 intermetallic phases. A specification condition the scope does not carry is reported outside it.
Why do ferrite content and intermetallic phases matter in super duplex stainless steel?
Super duplex stainless steel resists corrosion only when its ferrite and austenite are in balance and its structure contains no sigma or other intermetallic phases, which form when heat treatment or welding goes wrong. ASTM E562 measures the ferrite fraction and ASTM A923 detects detrimental intermetallic phases; EIL 6-79-0015 calls for both checks.