
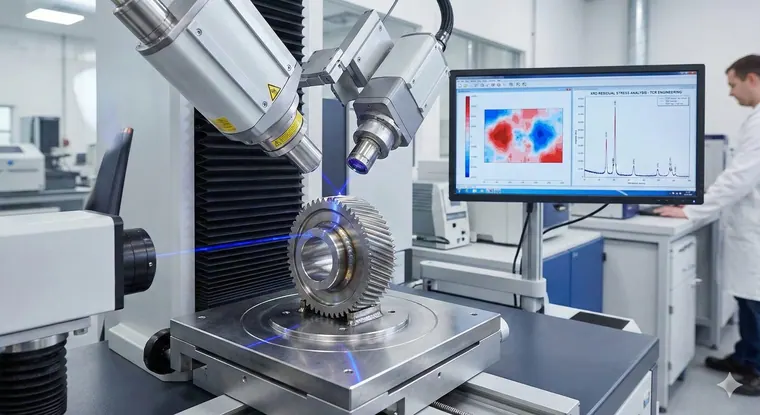
TCR Engineering measures residual stress by X-ray diffraction (XRD) at its Mahape laboratory in Navi Mumbai, India, using the sin-squared-psi method of ASTM E2860. The test is non-destructive and reads surface and near-surface stress in welds and in machined, ground and shot-peened metal parts. Residual stress by XRD is reported outside the NABL scope of certificate NABLT0726MH18640.
- Standard: ASTM E2860, sin-squared-psi method
- Parts: welds, machined and ground surfaces, shot-peened and heat-treated components
- Accreditation: reported outside the NABL and NADCAP AC7101 scopes
- Sample size and schedule: stated in the quotation
Ever wondered why that critical component failed unexpectedly despite passing all quality checks? Or why identical parts from the same batch sometimes behave differently under stress? The answer often lies hidden in something you can't see with the naked eye: residual stresses. Manufacturing processes like welding, machining, grinding, and heat treatment leave invisible footprints inside materials. These internal stresses can make or break your component's performance, literally. That is where TCR Engineering conducts residual stress measurement using X-ray Diffraction (XRD) to give you the insights you need.
Why Residual Stress Measurement Matters (And Why You Should Care)
Think of residual stress as the silent saboteur in your manufacturing process. Here is what happens when you ignore it:
- Components crack during service without warning
- Fatigue life gets drastically reduced
- Corrosion accelerates in unexpected areas
- Dimensional stability goes out the window
Industries like aerospace, automotive, power generation, and oil & gas have learned this the hard way. One aerospace manufacturer discovered that grinding marks on turbine blades created tensile residual stresses that led to premature fatigue failures, at a heavy cost in recalls and reputation.
What Makes X-ray Diffraction the Smart Choice?
Unlike destructive testing methods that require you to sacrifice samples, XRD is non-destructive. Your components remain intact and usable after testing. It is like getting an MRI for your parts instead of exploratory surgery.
The technique works by measuring how X-rays diffract off the crystal lattice of your material. When residual stresses are present, they distort this lattice, and XRD picks up these microscopic changes.
Key advantages:
- Non-destructive nature preserves your expensive components
- Surface and near-surface stress measurement capabilities
- Measurement uncertainty stated in the report
- Works on a wide range of metallic materials
- Portable equipment options for field measurements
TCR Engineering's XRD Service: What You Need to Know
Three points decide how a measurement is planned: the sample, the schedule and the accreditation status.
Sample Requirements That Work for Real-World Testing
TCR Engineering has designed its XRD residual stress measurement service with practicality in mind. The preferred sample dimensions are stated in the quotation, and they cover most component testing needs. Flat samples work best, though the team can often accommodate slightly curved surfaces with proper fixturing.
Sample too large? That is a conversation worth having. Sometimes sectioning strategies or on-site measurements can solve size challenges. The key is getting in touch early in your project planning phase.
Planning the Schedule
TCR Engineering confirms the schedule in the quotation. The schedule covers:
- Sample preparation and surface cleaning
- Multiple measurement points, as the enquiry needs
- Data analysis and stress calculation
- Comprehensive report generation
Understanding the Accreditation Status
Transparency matters. Residual stress by XRD is reported outside the NABL scope of certificate NABLT0726MH18640. What does this mean for you? NABL (National Accreditation Board for Testing and Calibration Laboratories) accreditation is crucial for regulatory compliance in certain industries. However, non-accredited testing still provides valuable technical data for:
- R&D and process development work
- Internal quality control programmes
- Failure analysis investigations
- Process optimisation studies
- Academic research projects
If your application requires NABL-accredited reports for compliance or certification purposes, discuss this upfront. TCR Engineering can guide you towards appropriate alternatives or partner laboratories when regulatory requirements demand it.
Real-World Applications Where XRD Makes a Difference
Residual stress measurement earns its place in three kinds of work.
Welding Process Validation
A pressure vessel manufacturer was experiencing random failures in field-welded joints. Using XRD residual stress measurement, TCR Engineering identified excessive tensile stresses near the weld toe. The solution? Modifying the welding sequence and introducing post-weld stress relief. Failures fell sharply.
Shot Peening Verification
Shot peening introduces beneficial compressive stresses to improve fatigue life. But are your peening parameters optimal? XRD measurement confirms whether you are achieving the target stress profile or just wasting compressed air.
Machining Process Optimisation
High-speed machining can introduce detrimental tensile stresses. One automotive component supplier discovered their cutting parameters were creating stress concentrations that shortened component life. XRD measurements helped optimise feeds, speeds, and tooling to flip those stresses from tensile to compressive.
How to Prepare Your Samples for Testing
Useful results start with proper sample preparation. Here is what helps:
Surface condition matters: Clean surfaces free from oils, scale, or coatings give the best results. The X-rays need to interact with the actual metal surface, not contaminants.
Document your processing history: Share details about manufacturing processes, heat treatments, and service history. Context helps interpret the stress measurements meaningfully.
Mark measurement locations: If you have specific areas of interest (like near a crack initiation site), clearly mark them. Random measurements might miss the critical zones.
Consider sectioning strategy: For large components, think through where to section and how to minimise disturbing the stress state during cutting. Water jet or EDM cutting typically works better than abrasive methods.
Making Sense of Your XRD Results
Your test report will include stress values (typically in MPa), measurement uncertainties, and often graphical representations of stress distribution. But what do these numbers actually mean?
Tensile stresses (positive values): Generally undesirable, these can accelerate fatigue crack initiation and propagation. Think of them as opening forces trying to pull the material apart.
Compressive stresses (negative values): Usually beneficial, these resist crack formation and growth. They are like a pre-load that external forces must overcome first.
Magnitude matters: A modest tensile stress might be negligible in a high-strength steel but critical in a sensitive aluminium alloy. Context is everything.
The TCR approach here is simple: don't just collect data, make decisions with it. Use these measurements to validate processes, troubleshoot failures, and optimise manufacturing parameters.
Integrating XRD Measurement into Your Quality System
Smart manufacturers don't use residual stress measurement as a one-off troubleshooting tool. They build it into their process qualification and periodic verification programmes. Consider these integration points:
New process qualification: Establish baseline stress profiles for qualified processes
Periodic process verification: Confirm that manufacturing processes remain in control
Failure investigation: Include stress measurement in your root cause analysis toolkit
Supplier qualification: Require stress documentation for critical purchased components
R&D validation: Verify that design changes deliver the intended stress state
When Does XRD Residual Stress Testing Make Sense?
The decision framework is straightforward:
High value: Critical components where failure consequences are severe (safety-critical parts, expensive assemblies, high-volume production)
Medium value: Process development work where you are establishing optimal parameters
Lower value: Well-established processes on non-critical components with good field history
Think of it as insurance with diagnostic capability. You are measuring what is actually happening inside your material, not guessing from process parameters.
Beyond XRD: Complementary Testing Services
Residual stress measurement often works best as part of a broader material characterisation programme. TCR Engineering offers related services that complement XRD analysis:
- Metallographic examination to understand microstructure-stress relationships
- Hardness testing to correlate mechanical properties with stress states
- Failure analysis services that integrate stress measurement with fractography
- Material testing capabilities for comprehensive component evaluation
Getting Started with TCR Engineering's XRD Service
The process is straightforward:
Initial consultation: Discuss your requirements, sample configuration, and testing objectives
Sample submission: Send components with clear marking of measurement locations
Testing and analysis: TCR Engineering conducts measurements and processes data
Report delivery: Receive comprehensive documentation on the date confirmed in the quotation
Technical discussion: Review findings and discuss implications (optional but recommended)
Ready to get started? Contact TCR Engineering's technical team to discuss your specific residual stress measurement needs.
The Bottom Line
Manufacturing in competitive markets demands control not just of dimensions but of the internal state of your materials. TCR Engineering conducts residual stress measurement using X-ray Diffraction (XRD) to give you that measurement. Whether you are troubleshooting unexpected failures, validating new processes, or optimising existing manufacturing methods, XRD residual stress measurement provides the data you need to make informed decisions.
With practical sample size requirements and engineering analysis, it is an accessible tool for quality-focused manufacturers. The question isn't whether residual stresses exist in your components: they always do. The question is whether you are measuring them, understanding them, and controlling them. That is where TCR Engineering comes in.
Frequently Asked Questions
What uncertainty does an XRD residual stress measurement carry?
The measurement uncertainty is stated in the report. It depends on material properties, grain size and texture, surface condition, and measurement parameters.
Can XRD measure through coatings or paint?
No, XRD requires access to the base material surface. Coatings must be removed from the measurement area without introducing additional stresses (chemical stripping works best).
What materials can be tested with XRD?
Most metallic materials with a crystalline structure work well, including steels, aluminium alloys, titanium alloys, and nickel-based superalloys. Amorphous materials and plastics aren't suitable for this technique.
How deep does XRD measure?
XRD is primarily a surface technique: it measures stress in a thin surface layer whose depth depends on the material and the X-ray radiation used. For depth profiling, layer removal techniques can extend this range.
What is the minimum sample size for testing?
The preferred sample dimensions are stated in the quotation, and smaller samples can often be accommodated with specialised fixtures. Discuss your specific geometry with the team.
Can measurements be taken on assembled components?
Sometimes, yes. It depends on geometry and access to the measurement locations. The XRD equipment needs proper positioning relative to the surface, which can be challenging with complex assemblies.
How should I store samples before testing?
Keep samples clean and dry at room temperature. Avoid mechanical damage to surfaces and minimise handling of measurement areas. If samples are from field failures, preserve as-received condition.
What information should I provide with my samples?
Include material specification, processing history (heat treatment, surface finishing, welding, etc.), service history if applicable, and specific measurement location preferences. The more context, the better.
Is XRD residual stress measurement NABL accredited?
No. TCR Engineering measures residual stress by X-ray diffraction to ASTM E2860 at its Mahape laboratory, and the test is reported outside the NABL scope of certificate NABLT0726MH18640 and outside the NADCAP AC7101 scope. The report names the method and gives the result as a measurement made outside the accredited scope.